
That shortcut is no longer good procurement practice.
The relevant question is not where a truck is made. It is whether the manufacturer has the engineering depth, production discipline, component strategy, validation capability and UK support structure to deliver performance in your application. For a growing number of senior fleet buyers, the answer from leading Chinese manufacturers is now an emphatic yes.
Chinese manufacturing has moved from capacity to capability
China’s largest industrial-vehicle manufacturers are not small assemblers competing simply by fitting fewer features. They are substantial engineering businesses producing electric counterbalance, warehouse, IC and increasingly automated equipment at scale. That scale matters: it funds dedicated production facilities, automation, product development, testing, quality systems and supplier relationships that can be difficult to replicate in fragmented, low-volume supply chains.
It also supports a faster learning cycle. When a manufacturer builds across many applications and markets, field experience feeds back quickly into the next product generation. Electric drivetrains, lithium-ion integration, telematics and operator-focused design are no longer exclusive territory for the historic premium brands.
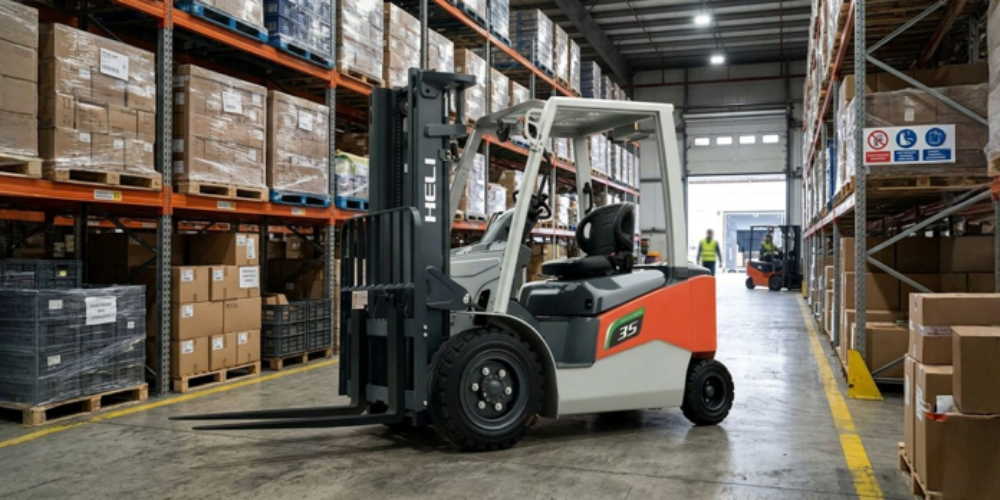
For buyers, this does not mean every Chinese product is equal. It means the category should be assessed properly. Look at the manufacturer, its engineering resources, the specification offered, evidence of performance in comparable duty cycles, parts availability and the competence of the UK support partner. A leading global producer such as HELI should be judged on those fact, rather than an outdated assumption.
A useful market signal: established brands are following the manufacturing strength
The market itself is providing an important clue. Well-known European manufacturers are increasingly using Chinese production, sourcing and partnerships to create value-oriented ranges and expand their electric portfolios. Jungheinrich, for example, confirms that its AntOn range is produced by strategic partner EP Equipment in Anji, China. That is not a criticism of its approach; it is a pragmatic acknowledgement that modern Chinese manufacturing can provide credible quality, speed and competitiveness for mainstream applications.
The takeaway for a fleet buyer is broader than one brand or one partnership. The debate has moved on from “Can China manufacture a capable truck?” The more useful question is: “Which manufacturer has designed the right truck for my operational demand, and which supplier can support it throughout its life?”
Do not confuse a familiar badge with the right product architecture
Every manufacturer has to make choices. A value-focused model may be built to a narrower application window, with fewer configuration options or a simpler component set than the flagship range. That can be entirely appropriate for light, predictable work. It becomes a problem only when a buyer assumes a familiar badge automatically means the product has the same capability as the premium model it resembles.
That is why the specification conversation must come before the price conversation. A fleet intended for multi-shift warehouse work, uneven external yards, ramp use, cold-store operation or demanding attachments needs to be assessed against its actual duty, not simply against a monthly figure.
At Grant Handling, our position is straightforward: value should come from fit-for-purpose engineering, efficient supply and accountable support, not from stripping out the capability your operation needs.
The cost base behind a quotation matters
Senior buyers are right to consider the resilience, service capacity and technical depth behind a supplier. They should also recognise that those benefits are delivered through different business models.
Some traditional premium organisations were designed around highly specified equipment, extensive branch networks and long-established cost structures. Their capability can be valuable where the application genuinely needs it. But when the requirement is a mainstream, high-utilisation fleet, an integrated manufacturer-and-distributor model can often bring a different balance: modern full-capability equipment, direct UK stock, a focused support structure and a sharper whole-life commercial proposition.
This is not an argument for buying the lowest-price truck. It is an argument for understanding what you are paying for—and ensuring the product, support and commercial model are aligned to the work being done.
A better evaluation framework for executive buyers
When reviewing a new purchase or rental fleet, ask suppliers to demonstrate five things:
- Application fit: What duty cycle, load centre, lift height, ground condition, attachment use and operating environment has the truck been specified for?
- Product capability: What is standard, what is optional and what differs from the manufacturer’s higher-specification range?
- Uptime plan: What is held in UK stock, how is parts availability measured and what service response is committed?
- Whole-life commercial case: Include energy, planned maintenance, tyres, damage exposure, replacement cover and residual/renewal assumptions—not merely the acquisition price.
- Accountability: Who owns the result when the fleet is under pressure: manufacturer, finance provider, dealer or one accountable partner?
The Grant Handling and HELI proposition
HELI brings the scale and capability of a major global industrial-vehicle manufacturer. Grant Handling brings the UK stockholding, application knowledge, service support and commercial flexibility that turns a product into an operating solution.
For customers, that means a credible alternative to badge-led procurement: equipment engineered for modern operational demand, specified around the job, supplied at pace and supported for the long term.
The best fleet decision is not about choosing “premium” or “value”. It is choosing the right level of engineering and support for the work and paying for capability that genuinely earns its place in the operation.


